
Every buyer has faced the frustration of a bulk shipment failing to match the “Golden Sample.” This gap between prototype perfection and mass production isn’t accidental, but a byproduct of transitioning from manual craftsmanship to high-speed industrial automation.
This article examines the systemic causes of quality drift, from process scaling and material optimization to psychological biases in the approval stage. We explore essential ISO-aligned frameworks and pre-production protocols to ensure consistency from the first prototype to final delivery.
Difference Between Hand-Made and Production Samples
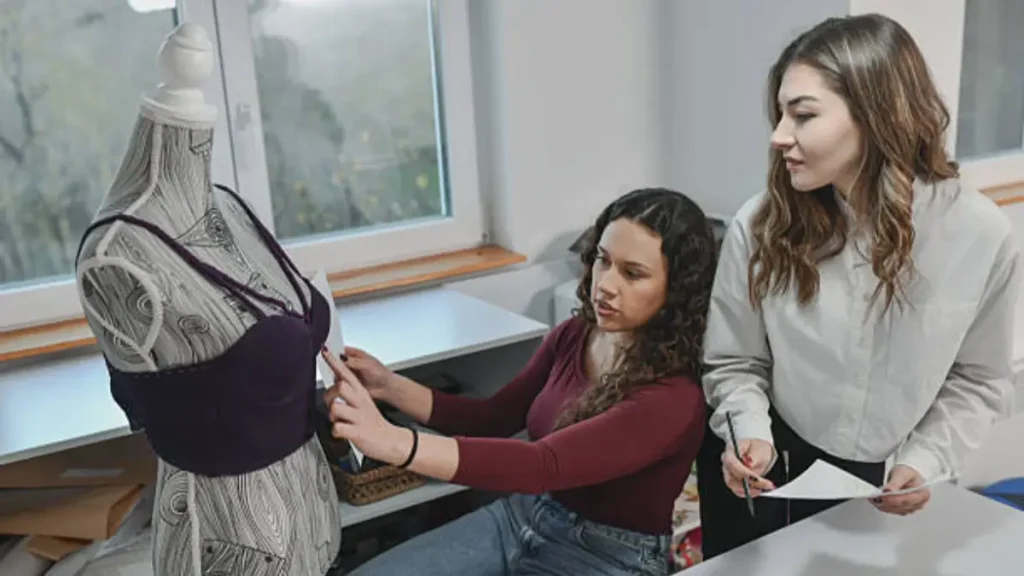
The transition from a “Golden Sample” to a full production run is a shift from artisanal precision to industrial efficiency. While prototypes focus on design perfection, mass production is governed by the constraints of high-speed automation and cost optimization.
Engineering Differences in the Manufacturing Cycle
The Prototyping Phase: Hand-made samples utilize a 1.5 cm seam allowance, providing the “buffer” needed for manual fit adjustments and silhouette refining. This stage prioritizes technical feasibility over cost.
The Production Phase: Patterns are “locked” and seam allowances are reduced to 1.0 cm. This 0.5 cm reduction is a strategic move to optimize fabric yield and nesting efficiency, directly reducing material waste across thousands of units.
The Quality Shift: Manual craftsmanship allows for real-time correction, whereas automated lines prioritize uniformity and cycle time, often smoothing over the artisanal nuances found in the initial sample.
Comparative Analysis: Sample vs. Batch
| Feature | Hand-Made Prototype | Mass Production Run |
|---|---|---|
| Output Volume | Typically 1-off “Golden Sample” | Hundreds to thousands of units |
| Seam Allowance | 1.5 cm (5/8″) for fit adjustments | 1.0 cm (3/5″) for fabric optimization |
| Quality Control | Manual, meticulous craftsmanship | Automated systems and standardized checks |
| Primary Objective | Design validation and feasibility | Scalability, speed, and cost-efficiency |
Material Substitutions and Cost Pressures
Strategic material substitution is a primary cause of quality disparity. While the “Golden Sample” uses premium components, mass production is often a “financial optimization” designed to achieve an average 8.7% cost reduction. This shift creates significant hidden costs for buyers, as performance is often sacrificed for factory margins.
The real causes for these substitutions in mass production include:
- The Margin Gap: Manufacturers swap raw materials for alternatives that reduce not only the unit price but also labor and scrap rates across thousands of units.
- Switching Inertia: If a cheaper material is compatible with existing machinery, factories have a high incentive to switch mid-production to offset market price spikes.
- Technical vs. Aesthetic Compliance: Substitutes often meet basic safety codes but lack the specific tactile or aesthetic properties of the original prototype.
To protect your brand, it is essential to compare Chinese supplier quotes based on their Bill of Materials (BOM) transparency. Quality drift occurs when substitutions are tested for process efficiency rather than long-term durability. Without strict oversight, these subtle changes in texture and strength only become visible once the batch is delivered.
Process Scaling Differences
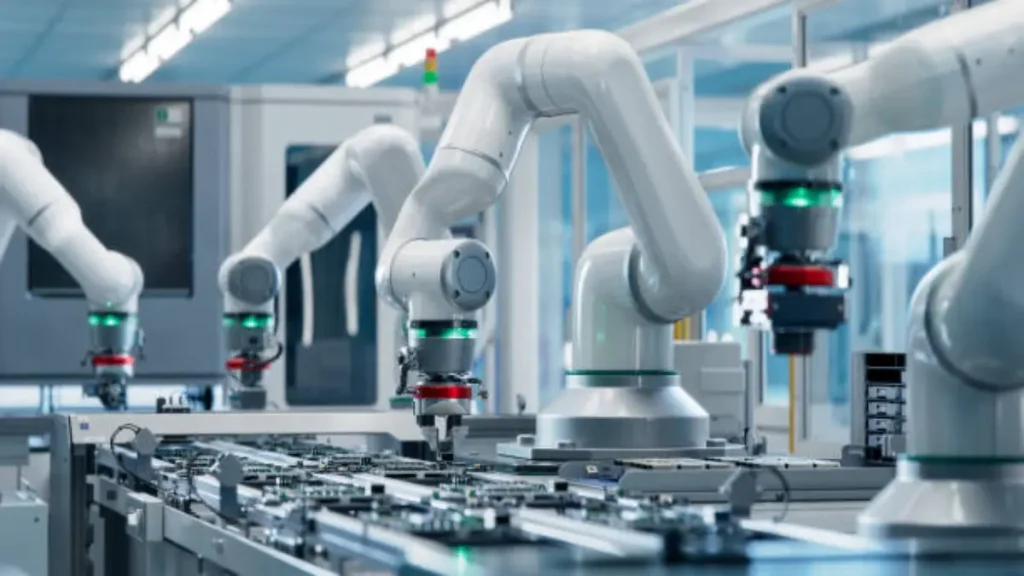
The transition from a controlled lab to a high-speed factory floor creates a technical gap. This hardware mismatch is a primary cause of quality drift in mass production.
Equipment Incompatibility
Samples are often made on low-speed, lab-grade machines. These lack the intense mechanical pressures and high-cycle speeds of industrial production lines, meaning the physical properties of the “Golden Sample” are technically difficult to replicate at scale.
The Nonlinearity of Volume
A 5-unit run is predictable, but a 5,000-unit cycle is volatile. Industrial machines run for longer durations, which causes heat accumulation and tool wear. This is why the MOQ in China often reflects the volume needed to stabilize these mechanical variables. Managing constant vibration and heat requires complex recalibration to maintain standards. These factors remain a core challenge in mass production quality control.
Data Insufficiency
Without physics-based data (e.g., precise PSI or micron-level tolerances), the first production run becomes a high-risk “live trial.” High-speed feeders and cutters alter material flow and shear resistance, causing the final product to deviate from the hand-crafted original.
To maintain consistency, brands must shift from “manual oversight” to automated process validation (ISO/ASTM standards) to catch mechanical drift before it ruins an entire batch.
Scale Your Brand with a Dedicated China Sourcing Partner

Quality Control Gaps Between Sample and Batch
The quality gap often stems from a fundamental shift in oversight. While a single sample receives 100% manual scrutiny, mass production relies on statistical probability, which allows defects to slip through.
Sampling Strategy Mismatch and Volume Stress
A single inspector cannot verify every unit in a high-volume batch. Traditional manual checks often fail because sampling frequency does not match production speed. Minor visual defects or measurement drifts escape detection during full-scale runs. This mismatch makes manual inspection methods obsolete for maintaining “Golden Sample” consistency.
Lack of Real-Time Statistical Process Control (SPC)
Sample creation masks process weaknesses through constant manual adjustments. In contrast, batch production requires Statistical Process Control (SPC) to detect trends early. Without in-line sensors and trend charts, minor variations quickly become major batch deviations. This lack of automated monitoring prevents factories from fixing issues before they escalate.
Absence of Systemic Root Cause Analysis
Consistency requires a shift from fixing symptoms to embedding quality. Robust systems must document every deviation with specific metadata like shift times and machine IDs. Without this data, the underlying drivers of production failure remain undiagnosed. This prevents manufacturers from aligning industrial output with the original technical specifications.
Emotional vs Technical Approval Bias
Many quality issues start at the approval desk. We often use our “feelings” about a sample instead of looking at hard data. Research shows a 50% probability that factors like cost and time will override technical quality during the final decision.
Emotional Trap: Being Blinded by the “Golden Sample”
When you hold a perfect sample, your brain wants to believe the entire batch will be identical. This is called “confirmation bias.” You focus on the beautiful finish but ignore small technical flaws that are hard to fix in mass production. This “visual perfection” acts as a psychological anchor. It masks risks like material inconsistency or weak structures that the sample simply doesn’t show.
Technical Compromise: When Deadlines Beat Standards
When you are in a rush to ship, your brain takes shortcuts. Data shows a 50% chance that project timelines will force you to ignore engineering specs. Even if a test shows a slight issue, you might approve it because the sample “looks good enough.” This “subjective buy-in” is dangerous. It means you are approving a product that works in a lab but will likely fail on a high-speed assembly line.
How to Align Sample Standards With Production
Aligning production with your “Golden Sample” requires moving from visual checks to technical engineering. By integrating ISO frameworks with data-driven tools, you can force the factory to replicate the prototype’s precision at scale.
Establishing the Quality Framework
The foundation of alignment is the ISO 9001:2000 standard. You must embed Plan-Do-Check-Act (PDCA) cycles into the production culture. This ensures every worker follows a systematic process rather than manual guesswork. Before bulk manufacturing starts, define Critical-to-Quality (CTQ) criteria on every drawing. These specs act as the “technical law” that raw materials and final assemblies must obey to ensure functional compatibility.
Technical Calibration and Live Monitoring
Consistency depends on accurate measurement. All testing instruments must follow strict calibration schedules to avoid data bias. Use Statistical Process Control (SPC) and Pareto Charts to track production in real-time. These tools help engineers catch “quality drift” before it ruins the whole batch. Furthermore, perform a Root Cause Failure Analysis (RCFA) for any deviation. This fixes the physics-based origin of the problem, such as mold wear or tool vibration, ensuring a permanent solution.
Essential Quality Alignment Tools
| Quality Framework | Technical Tool | Primary Purpose |
|---|---|---|
| ISO 9001:2000 | PDCA & TQM | Standardizes quality management systems to align production with specs. |
| Statistical Control | SPC & Pareto Charts | Identifies and prioritizes real-time quality deviations. |
| Material Verification | TAPPI Chart & CTQ | Ensures raw materials meet particulate and functional requirements. |
The “First Piece” Verification Gate
Always mandate a formal “First Piece” production run. This involves testing the very first units coming off the mass production line after setup. It verifies that the machinery, safety protocols, and worker ergonomics are correctly aligned with the sample.
When to Use Preproduction Samples
The PPS is your final safety net. You should implement it after prototype approval but before flipping the “on” switch for bulk manufacturing. It acts as the bridge between a theoretical design and a stable industrial process.
The Strategic Timing
You must insist on a PPS when transitioning from a master tailor’s hands to a high-speed assembly line. While your initial “Golden Sample” was likely made in a quiet studio, the PPS is produced using the actual machinery, trims, and staff assigned to your order. This is the only time to catch “process errors”—like fabric shrinkage under industrial heat—before they ruin your entire inventory.
The Decision-Making Milestone
Use the PPS as your final technical benchmark. This 10–14 day phase allows you to verify sizing consistency (Size Sets) and color matching under factory conditions. Once signed, the PPS serves as a binding contract. It gives your quality inspectors a physical standard to hold against the final shipment, ensuring that “mass-produced” never means “lower quality.”
Final Thoughts
To bridge the quality gap, you must treat the “Golden Sample” as a technical blueprint rather than just a visual goal. Success at scale is not a matter of luck; it is the result of replacing subjective approval with rigorous ISO standards and stable industrial processes.
Navigating these complexities requires a professional sourcing agent on the ground. At ASG, we verify Chinese factories and enforce strict PPS protocols to ensure your mass production matches your prototype. Explore ASG products!
Stop leaving your quality to chance—let us secure your supply chain.
Frequently Asked Questions
Why do samples often look better than bulk production orders?
Samples are hand-crafted prototypes designed for testing and approval, allowing for individual craftsmanship and adjustments. Bulk production prioritizes speed and cost efficiency through standardized workflows; this shift from customization to high-volume standardization is the primary reason for quality variance.
Are manufacturing samples actually hand-made?
Yes, samples involve significantly more manual, individualized labor compared to bulk production. They are sewn with high attention to detail to allow for pattern refinements, whereas bulk production follows a rigid, fixed design using standardized machinery and processes.
What is the role of a Pre-Production (PP) sample in quality control?
The approved PP sample serves as the definitive production blueprint. It acts as the reference standard for the factory, ensuring that quality assurance teams have a physical benchmark to match against bulk units for consistency in construction, labeling, and materials.
How can buyers prevent quality gaps between the sample and the final shipment?
Buyers should conduct thorough durability and shrinkage testing before sign-off, clearly communicate all changes before the PP stage, and utilize Top of Production (TOP) samples—units pulled directly from the mass production line—to verify that the final output matches the golden sample.
What are common quality issues that arise when scaling to mass production?
Common issues include uneven seams, incorrect label placement, and inconsistent fabric drape. These typically occur because the intensive individual attention given to a single sample is replaced by high-speed assembly lines where variability increases across hundreds or thousands of units.





